Confined Heavy Lift · Shaft Assembly · One-Directional Sequence
Assembling the World's Largest Tunnel Boring Machine — at the Bottom of a Pit
By Marco Torri · Founder and Editor, EE&HL Network
Seattle, USASR 99 TunnelAssembled 2013
A large tunnel boring machine is never lowered into the ground in one piece. It is built there — one confined heavy lift at a time, at the bottom of a shaft where there is almost no room left to correct a mistake once assembly has begun.
Bertha, built by Hitachi Zosen for Washington State DOT's SR 99 tunnel beneath Seattle, is the clearest documented example of what that constraint actually looks like in practice. At 17.5 m in diameter, it was, at the time, the largest earth pressure balance tunnel boring machine ever built — and every stage of getting it into the ground was governed by transport limits and shaft geometry, not by what would have been easiest to assemble.
17.5 m
Cutterhead diameter
41
Delivered sections
745–944 t
Cutterhead weight (reported range)
~80 ft
Launch pit depth
Stage 1
Transport-governed sectioning
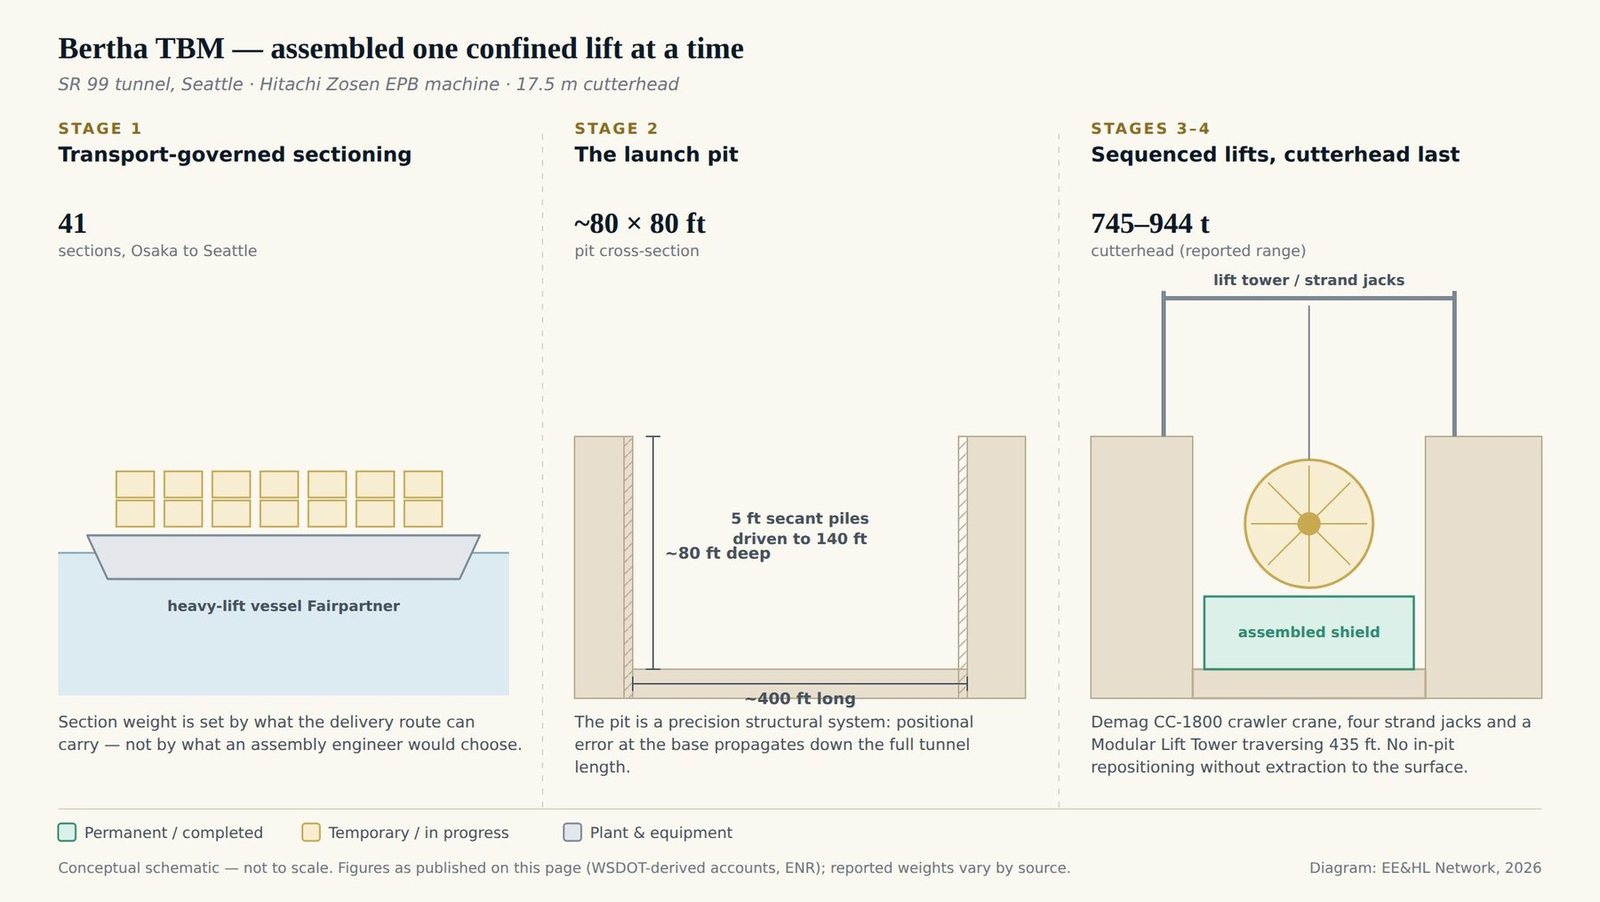
Bertha's total assembled weight — reported variously at 6,100, 7,000 and 7,982 tons across different sources — could never move as one unit. Hitachi Zosen built it at Osaka, Japan, then shipped it to Seattle in 41 separate sections aboard the heavy-lift vessel Fairpartner, operated by Jumbo. On large TBMs generally, section weight is set by the maximum load a delivery route can carry — typically 300–900 tons per piece — not by what an assembly engineer would otherwise choose.
Stage 2
The launch pit as a structural component
Bertha's launch pit measured roughly 80 ft wide, 80 ft deep and 400 ft long, built with 5-ft-diameter secant piles driven to 140 ft. On machines in this class, positional tolerance at the base of a 15–25 m shaft has to be held to millimetre-level precision — error at that stage propagates down the full tunnel length and cannot be corrected once boring begins. The pit is a precision structural system, not a staging area.
Stage 3
Sequenced component lifts
Components were lowered into the pit using a Demag CC-1800 crawler crane, four strand jacks of roughly 720 to 940 tons capacity, and a custom Barnhart-built Modular Lift Tower traversing 435 ft of the pit floor. Each lift was confined, with restricted headroom and no room to reposition a mis-rigged piece without extracting it back to the surface — a significant cost and programme setback on a machine this size.
Stage 4
The cutterhead, lowered last
Bertha's cutterhead — reported at 944 tons in WSDOT-derived accounts, though ENR's contemporaneous assembly coverage gives 745 tons — was lowered last, into a shaft with minimal remaining clearance around it. Once the rest of the machine was assembled beneath it, there was no option left to reposition the cutterhead if it came in misaligned; final geometry had to be right the first time.
Sequencing note
Assembly sequence on a machine like this is effectively one-directional. There is no practical way to extract a lower component, reposition the machine, or change the sequence once erection has advanced. If a fault surfaces after final assembly, it has to be diagnosed and corrected underground — not by reversing the erection sequence. Preparation replaces recovery as the governing engineering discipline.
A TBM is assembled at the bottom of a pit. Not lowered in one piece — built there, one confined heavy lift at a time.
Bertha launched on 30 July 2013 and completed its 9,270-ft drive beneath Seattle in 2017, four years and one well-publicised mid-tunnel repair after boring began. Whatever the individual figures in circulation for its total weight, the underlying discipline it demonstrates is consistent across large-diameter TBM assembly generally: the governing moment isn't the first metre bored, it's the last component landed — and every decision upstream of that, from cradle design to lift sequence, exists to get that one moment right.
The Bertha retrieval site in Seattle, July 2015: the red gantry crane (centre) lifted the cutterhead from a shaft dug in front of the stalled machine; the white shed (right) housed it during repairs. This shows the 2015 repair operation, not the original launch-pit assembly. Resized from the original for web display. Photo: SounderBruce, Wikimedia Commons, CC BY-SA 2.0.Bertha TBM — assembled one confined lift at a time. Diagram: EE&HL Network, 2026. Conceptual schematic — not to scale. Tap or click the diagram to open it full size.
Sources:ASME — comparative TBM dimensions; Bertha (tunnel boring machine) — manufacturer, assembly chronology and machine data. Bertha was the largest earth pressure balance TBM; larger-diameter slurry TBMs have since been built, and published weights vary between roughly 6,100 and 6,900 tonnes depending on configuration.
Frequently Asked Questions
Trade press and reference sources give inconsistent totals — figures of roughly 6,100 tons (Wikipedia), 7,000 tons (geoprac.net) and 7,982 tons (Tunnel Business Magazine) have all been published. All fall within the general range typical of large-diameter TBMs of this class; treat any single precise figure as approximate rather than settled.
No transport route could carry a machine of Bertha's total weight and diameter in one piece. It was built by Hitachi Zosen in Osaka, Japan, then shipped to Seattle in 41 separate sections aboard the heavy-lift vessel Fairpartner, operated by Jumbo — the same constraint that governs section sizing on large TBMs generally: components are sized to what the delivery route can carry, not to what would be most convenient to assemble.
Assembly took place directly inside the launch pit — roughly 80 ft wide, 80 ft deep and 400 ft long, built with 5-ft-diameter secant piles down to 140 ft. Components were lowered and positioned using a Demag CC-1800 crawler crane, four strand jacks of roughly 720 to 940 tons capacity, and a custom Barnhart-built Modular Lift Tower that traversed 435 ft of the pit floor — a confined, sequenced heavy-lift operation rather than a single crane pick.
Published figures differ: WSDOT-derived accounts cite the cutterhead at 944 tons, while ENR's contemporaneous assembly coverage gives 745 tons and reports the largest single modeled lift of the assembly at 1,250 tons. On large-diameter TBMs generally, the cutterhead is lowered last because it is one of the heaviest, least manoeuvrable lifts into a shaft with minimal clearance; once the rest of the machine is assembled beneath it, there is no room left to reposition a mis-rigged cutterhead without extracting it back to the surface.
In practice, no. Once major components are lowered and joined inside a shaft with only 1–2 metres of radial clearance on large machines, there is no option to extract a component or reposition the machine without significant crane cost and programme delay. A fault discovered after final assembly typically has to be diagnosed and corrected underground rather than by reversing the erection sequence — which is why preparation, not recovery, governs the engineering discipline for this type of assembly.
Commercial intelligence for erection engineering professionals
The EE&HL Network newsletter covers the decisions, constraints, sequences, and commercial patterns behind the world's most complex lifting and erection projects.